


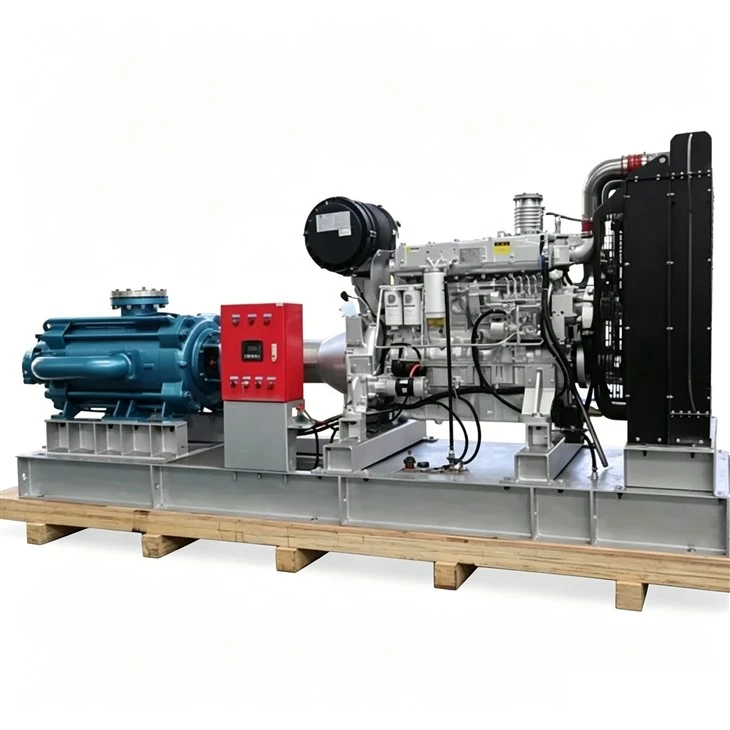

Diesel Engine Driven Mining Self-balancing Multistage Pump
designed for mine drainage, industrial dewatering, and long-distance water transfer applications.
Self-balancing design, durable, and requires no electricity. Get a quote now.
Description
Technical Parameters
Henan Yibeng Pump Industry Co., Ltd. is one of the leading manufacturers and suppliers of diesel engine driven mining self-balancing multistage pump in China. We have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy durable diesel engine driven mining self-balancing multistage pump at competitive price from our factory.
Diesel engine driven mining self-balancing multistage pump

The Diesel Engine Driven Self-Balancing Multistage Pump is designed for mining dewatering, high-head water transfer, and remote projects without electricity. Equipped with a self-balancing structure, this pump eliminates axial force issues common in traditional multistage pumps, ensuring longer service life, stable operation, and reduced maintenance costs.Powered by a reliable diesel engine, it is ideal for mining projects in Africa, the Middle East, and other off-grid environments.
Product Parameter
| Customized support | OEM, ODM, OBM |
| Power Source | Diesel engine |
| Brand Name | HNYB |
| Structure | Multistage Pump |
| Application | Industrial Boilers, Industrial Utilities, Irrigation and Agriculture, Mining industry, Raw Water Intake |
| Place of Origin | Henan, China |
| Power | 3-1600kw |
| Outlet Size | ≤300mm |
| Flow | 3.7-1350m³/ h |
| Head | 50-1800m |
| Material | Cast iron/ductile iron/cast steel/stainless steel |
Products Video

Typical Applications:
⛏️ Mining Industry
- Mine dewatering
- Underground water drainage
- Tailings water transport
- Emergency flood drainage
- Industrial wastewater transfer
- Coal mine drainage systems
- Remote mining site water supply
🚜 Remote Water Supply
- Off-grid water transfer
- Emergency water pumping
- Long-distance high-head water delivery
🌊 Industrial Applications
- High-pressure water systems
- Booster pumping stations
Self-Balancing Pump vs Traditional Multistage Pump
| Feature | Self-Balancing Pump | Traditional Pump |
|---|---|---|
| Axial Force Balance | Automatic | Balance Disc |
| Maintenance | Low | Frequent |
| Balance Water Leakage | No | Yes |
| Efficiency Stability | Excellent | Declines Over Time |
| Operating Reliability | High | Moderate |
| Service Life | Longer | Shorter |
Advantages
Advanced Self-Balancing Technology
- Unlike traditional multistage pumps using balance discs, the HNYB self-balancing pump adopts a symmetrical impeller arrangement to automatically offset axial thrust during operation.
- This advanced design reduces component wear, eliminates balance water leakage and improves long-term operating stability.
- The pump achieves higher hydraulic efficiency and lower maintenance costs under demanding mining conditions.
Reliable Diesel Engine Drive System
- The pump can be equipped with Cummins, Weichai, Perkins or other internationally recognized diesel engines for reliable off-grid operation.
- The diesel driven configuration is especially suitable for mining sites without stable power supply and emergency drainage applications.
- It provides stable high-pressure operation under harsh outdoor working conditions.
Heavy-Duty Industrial Construction
- The pump casing, impellers and hydraulic components are manufactured from high-strength wear-resistant materials for demanding industrial environments.
- Precision-balanced rotors and heavy-duty bearings ensure stable continuous operation with reduced vibration and extended service life.
Product Features
Self-Balancing Technology
- Eliminates axial thrust without a balance disc
- Reduces wear and maintenance
- Ensures long-term stable operation
- Ideal for continuous mining operations
Diesel Engine Driven – No Electricity Required
- Perfect for remote mining sites
- Compatible with leading diesel engine brands
- Easy to operate and maintain
High Head & Long-Distance Water Transfer
- Head up to 800 meters
- Multi-stage impeller design
- Suitable for deep mine drainage
Heavy-Duty Design for Harsh Environments
- Anti-corrosion materials available
- Designed for dust, heat, and continuous operation
Easy Maintenance & Long Service Life
- Fewer wear parts compared to traditional pumps
- Modular design for quick servicing
- Reduced downtime

Product Certification

ISO 9001

ISO14001

ISO45001

CE Product Certification

EAC Product Certification

Verified Supplier

Why Choose HNYB PUMPS
At HNYB PUMPS, we specialize in high-pressure multistage pump solutions for global industrial applications
30+ years manufacturing experience
Export to 100+ countries
Custom pump solutions for mining projects
Strict quality control & testing
Our address
Zhaogang Industrial Park, Fengqiu, Xinxiang, Henan, China
WhatsApp Number
+86 158 3619 1545
sales@hnybpumps.com

FAQ
01. Why choose a diesel engine pump instead of electric?
02. What is the advantage of self-balancing structure?
03. Can the pump be customized for mining conditions?
04. What diesel engine brands do you support?
05. CAN YOU DO OEM BRAND?
06. WHAT IS THE DELIVERY TIME?
Hot Tags: diesel engine driven mining self-balancing multistage pump, China diesel engine driven mining self-balancing multistage pump manufacturers
| Flow range: | 3.7~1350m³/h |
| Head: | 50~1800m |
| Caliber: | ≤300mm |
| Power: | 3~1600kw |
| Medium temperature: | -20℃~150℃ (need to explain if it is higher than 80℃) |
| Material: | Cast iron/ductile iron/cast steel/stainless steel, etc. |
| Scope of application: | Transporting clean water or special liquids that do not contain or contain a small amount of solid particles, mainly used for industrial, mining and urban water supply and drainage, pressurized water supply for high-rise buildings, garden sprinkler irrigation, fire pressurization, long-distance water delivery, heating, bathrooms and other hot and cold water circulation pressurization and equipment supporting etc. |
Send Inquiry


