
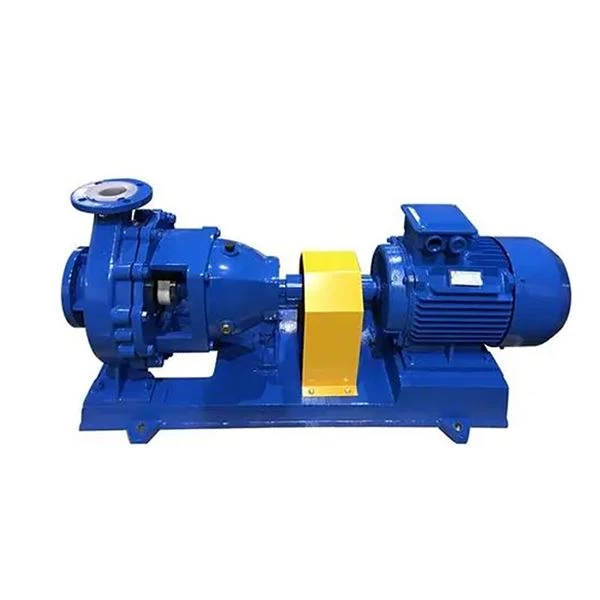


Chemical Resistant Centrifugal Pump
alkalis, and corrosive solvents. Available in PTFE, PVDF, and SS316L configurations.
Contact YB Pumps for chemical compatibility charts.
Description
Technical Parameters
Chemical Resistant Centrifugal Pump

The HNYB Chemical Resistant Centrifugal Pump is designed for transferring corrosive, aggressive and chemically active liquids in industrial process systems.
The pump can be configured with corrosion-resistant wetted materials, liners and sealing arrangements according to the chemical composition, concentration, temperature, pressure and solids content of the pumped liquid.
Depending on the application, suitable configurations may include fluoropolymer-lined, stainless-steel and corrosion-resistant alloy components.
Typical applications include chemical processing, petrochemical facilities, wastewater treatment, electroplating, pharmaceuticals and other industries where material compatibility is critical.
Product Parameter
| Customized support | OEM, ODM, OBM |
| Power Source | Electric |
| Brand Name | HNYB |
| Structure | Single-stage Pump |
| Application | Industrial Boilers, Industrial Utilities, Irrigation and Agriculture, Mining industry, Raw Water Intake |
| Place of Origin | Henan, China |
| Power | Choose according to the viscosity and specific gravity of the liquid |
| Outlet Size | ≤600mm |
| Flow | 5.5-1800m³/ h |
| Head | 16-1400m |
| Material | Cast iron/ductile iron/cast steel/stainless steel |
Products Video
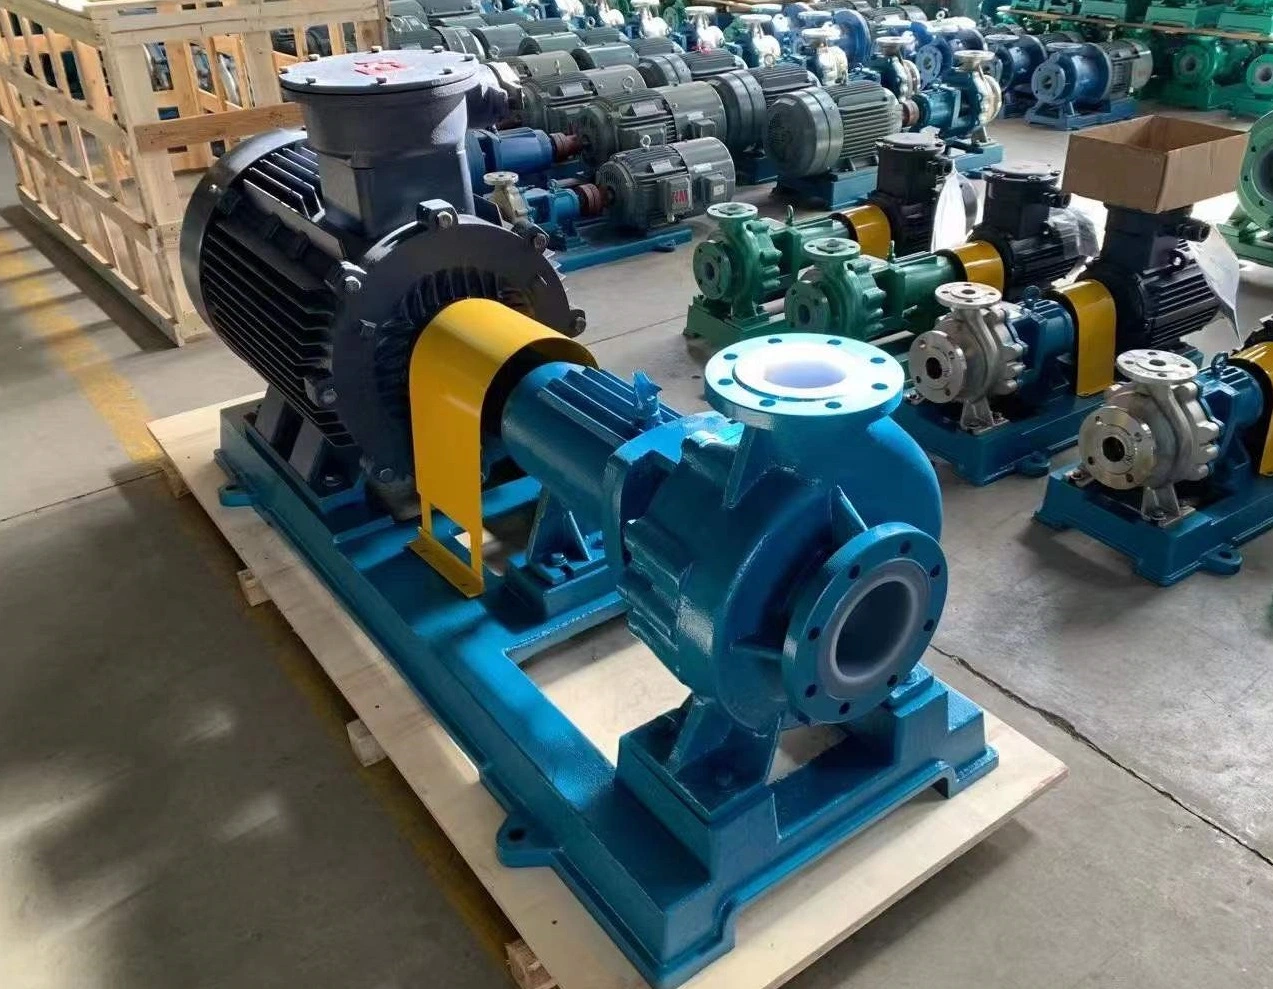
Application Scenario:
- Chemical Industry: Chemical-resistant centrifugal pump plays a vital role in the chemical industry and is used to transport various chemical liquids, including corrosive, high-temperature, high-pressure, flammable, explosive, and other difficult-to-handle media.
- Petroleum Industry: Chemical-resistant centrifugal pump is used to transport fluid media such as petroleum, refined oil, natural gas, etc., especially in every process link of the refinery, such as raw material transportation, commodity separation, catalytic reaction, etc.
- Metallurgy and Electric Power: In the metallurgical industry, chemical-resistant centrifugal pump is used to transport corrosive liquids and high-temperature melts produced in various metallurgical industries. In the power industry, chemical-resistant centrifugal pump is used in power station refrigeration systems, boiler water supply, and wastewater treatment.
Technical Matrix & Material Boundaries
To ensure perfect chemical compatibility, our engineering team assists you in selecting the ideal metallurgy or thermoplastic lining tailored to your medium's chemical concentration and operating temperature.
| Pump Material Option | Best Suited Mediums | Temperature Operational Limits |
|---|---|---|
| PTFE / PFA Lined | Strongest acids, aqua regia, chlorine solutions, and universal solvents. | -20°C to +120°C (-4°F to 248°F) |
| PVDF Polypropylene | Excellent for industrial wastewater, highly concentrated hot acids, and halogens. | -10°C to +90°C (14°F to 194°F) |
| SS316L / Duplex Stainless Steel | Organic acids, mild corrosive slurries, food-grade chemical transfers. | -40°C to +250°C (-40°F to 482°F) |
| Titanium / Hastelloy Alloy | Extreme high-temperature brines, marine chemistry, and localized high-chloride liquids. | Up to +350°C (Custom engineering) |
Product Features
High Chemical Resistance: Chemical-resistant centrifugal pumps are designed to handle a wide range of aggressive chemicals and fluids, including acids, bases, solvents, and other corrosive substances.
Durable Construction: These pumps are typically made of high-quality materials that resist chemical corrosion. Their advanced design ensures advantages such as corrosion resistance, tight sealing, low noise, and long service life.
Versatility: Chemical-resistant centrifugal pumps can be used in a variety of applications in industries such as chemical processing, pharmaceuticals, food and beverage, and water treatment.
Energy Efficiency: These pumps are designed to operate efficiently, which reduces energy costs and environmental impact.
Low Maintenance Costs: Chemical-resistant centrifugal pumps require minimal maintenance costs because they are designed to withstand harsh chemical environments without corrosion or deterioration.
Reliable Performance: These pumps provide reliable performance, ensuring that processes can run smoothly without interruption or damage.
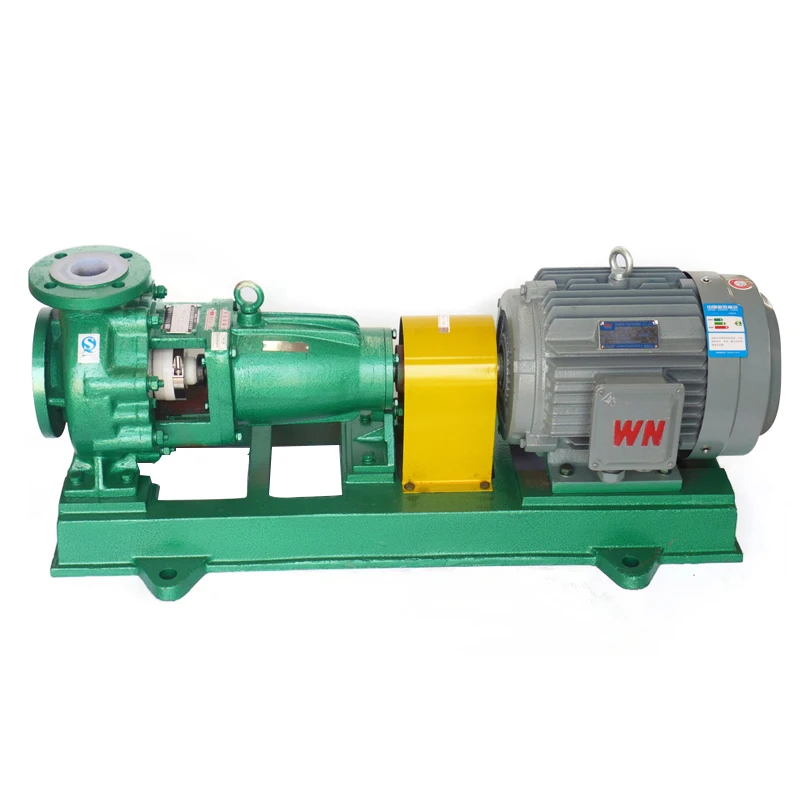
Your OEM Partner for Industrial Chemical Safety
HNYB PUMPS provides comprehensive technical backing and regulatory compliance for global chemical plant distributors and infrastructure engineers:
100% Material Traceability Certifications: Full EN 10204 3.1 material certificates are supplied for all alloy and metallic casings to ensure strict environmental auditing.
Explosion-Proof Motor Standards: All chemical pump units can be packaged with ATEX, IECEx, or NEMA-compliant flameproof/explosion-proof electric motors for hazardous zone placement.
Custom Hydrostatic Expansion Testing: Every chemical pump casing undergoes rigorous pressurized holding tests to guarantee absolute structural integrity before leaving the factory floor.
Product Certification

ISO 9001

ISO14001

ISO45001

CE Product Certification

EAC Product Certification

Verified Supplier
Our address
Zhaogang Industrial Park, Fengqiu, Xinxiang, Henan, China
WhatsApp Number
+86 158 3619 1545

FAQ
01. WHAT'S YOUR MOQ?
02. WHAT'S YOUR PAYMENT TERMS?
03. WHAT CERTIFICATES DO YOU HAVE?
04. ARE YOU A MANUFACTURING OR TRADING COMPANY?
05. CAN YOU DO OEM BRAND?
06. WHAT IS THE DELIVERY TIME?
Hot Tags: Chemical Resistant Centrifugal Pump, China Chemical Resistant Centrifugal Pump manufacturers
Product parameters
| Flow Rate(Q): | 5.5~1800m³/h |
| Head(H): | 16~1400m |
| Pressure: | 0.16MPa~14MPa(1.6Bar~140Bar) |
| Power: | According to the viscosity and specific gravity of the liquid. |
| Liquid Temperature: | -80°C~450°C(-112°F~842°F) |
| Material: | Cast Steel/Stainless Steel/Heat Resistant Steel, Etc |
| Scope of application: | used to transport low-temperature or high-temperature liquids, neutral or corrosive liquids, clean or liquids containing solid particles, liquids that are not allowed to be contaminated, etc. Suitable for chemical industry, oil refining, papermaking, sugar refining, food, pharmaceuticals, synthesis Fiber and other industries. |
Send Inquiry


